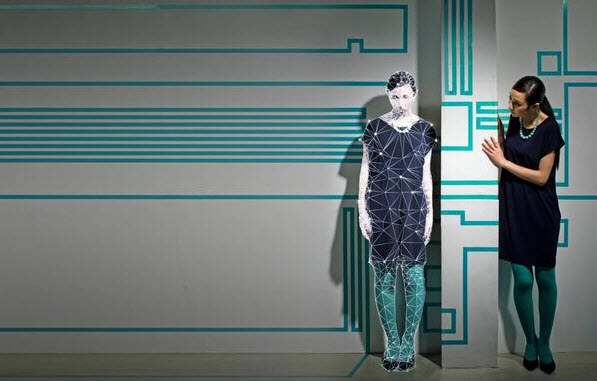
The Digital Twin approach to virtual product development has been successful in industries such as automotive and electronics, each with long established and standardised ways of modeling product components, end-use requirements, and manufacturing processes. A proven framework is available for the apparel industry to follow. However, unlike those other industries, the apparel industry deals with materials that are flexible, not rigid. Before apparel brands can move to the MetaVertical process, digital twins must be developed to model the appearance and performance of the flexible fabrics used to make garments, as well as garment end-use requirements and manufacturing processes. With those prerequisites in place, brands will be able to adopt radically faster processes to incorporate and manage the entire apparel supply chain.
The World Economic Forum (WEF) stated, ‘Data is the new oil’ and we believe this is true, understated and is an imperative mindset that must be adopted in the factory of the future. WEF has recently come to the conclusion that data has major differences from oil in that oil is a single use commodity and is scarce while data can be used many times and its growth is exponential (Schlosser, 2018). In the garment factory, where could this data come from and what do we do with it?
Black Swan Textiles, a digitalisation consultancy in the apparel industry, is dedicated to developing the digital twin in apparel. We have a very clear vision of what the factory of the future looks like and, as stated in a previous blog post, Understanding the Apparel Digital Twin, “A factory utilising the digital twin methodology has modeled all manufacturing equipment, operators, and processes, enabling it to simulate the operations necessary to assemble any particular product.” Once this virtual environment is established, we are then able to implement the systems, processes and machines that we have commissioned in a virtual environment. Although plant and process simulation are extremely beneficial, this is merely the beginning of the digitalisation journey.
Digital twin
SCADA
It starts with the machines and devices on the factory floor and in many garment factories around the world we rely on human operators and the machines remain disconnected from the enterprise and shopfloor control systems. This must evolve and become standard. Once proprietary, machine builders and manufacturers have begun to understand that these machines and systems benefit from open communication to other machines for the end users benefit. Once connected, the overarching system that connects them to each other. Supervisory Control and Data Acquisition (SCADA) systems are standard on the factory floor for many batch-process and discrete-parts manufacturing industries including food and beverage, pharmaceutical, oil and gas, etc.
When SCADA, recipe management systems, ERP, MES and other enterprise systems work together on a common set of goals it creates a train of planning, production, quality, shipping and finance that is quite powerful. Recipe management is a complex system in the apparel industry and made simpler if we have a fully engineered product digital twin and control system on the factory floor. With the product’s digital twin and the control system implemented we can then produce product based on the individual components needed and based on what the design has very specifically called for. Those individual components can now be distributed to the individual machines and workstations required to assemble the garment. The output data from these processes will then begin to optimise product quality based on standards and thresholds predefined by the brand.
MES
We then need to also consider connecting production machines, SCADA and business systems to an intermediary that can receive and distribute these order details for optimised workflow and manufacturing processes. Manufacturing Execution Systems (MES) have been adopted and used in many industries, including automotive and pharmaceutical, and when implemented can create, organise and act on massive amounts of data on the factory floor and the business systems to optimise production efficiency.
There are many facets and benefits to an MES system deployment for the manufacturer. The ability to collect historical data, predict future production bandwith, monitor employee and machine performance in real time are tremendous benefits that will optimise the way products are brought to market with your customers and suppliers. This production loop between systems and machines is incredibly powerful for continuous improvement of garment quality, speed to market and worker efficiency.
Insight and advanced analytics
We have now created, acted on and leveraged data from the factory floor and MES. The Fourth Industrial revolution is upon us and provides the technology to allow us to do so much more with that data than we could in the past. Machine learning and scalable cloud/edge computing puts this data into overdrive to improve production performance in near real time.
Due to the fragmented nature of the apparel industry, it is very difficult to share the right data with the right companies to drive the right results. By leveraging the cloud we now have a way to distribute meaningful information to for real time analysis and decision making. Blockchain technology is inherently more secure due to its use of cryptography and the imutability of the data that is published to the blockchain network. With the implementation of a permissioned based Blockchain network all members would have the ability to publish data and access stored records that reside on a decentralised system that is virtually risk free from hackers.
By creating and publishing data directly from our SCADA and MES systems to ‘apps’ in the cloud we now have the ability to make decisions from our mobile devices, tablets and other connected components. This isn’t just connectivity and alarming though, this is the ability to receive insights into the current and future states of our production and supply chains performance.
What if we could predict the future?
In the past, it was common place to get vehicles oil changed every 3,000 miles because that’s what manufacturers told us was the recommended schedule. Now we have the ability for the vehicle to monitor the engine and oil and alert the driver when an oil change will be needed in the near future, before damage occurs. By predicting when this maintenance is required, we then are able to plan when the maintenance should be performed rather than relying on a legacy schedule, thus keeping us on the road longer. This is no different in manufacturing, unplanned downtime costs factories many valuable resources.
The ability to predict anomalies in the product and manufacturing processes will dramatically improve speed to market and the quality of the product. For example, historically product inspections and rework have cost factories time and money. Get it right the first time, with assurances from the systems you have in place plus the anomaly detection algorithms that predict when something undesired will occur. The inefficient time spent on quality is near its end as the industry adopts inline quality systems and cloud-based software platforms that will replace these manual processes that take days or weeks to get right, thus costing significant resources.
How do the brands benefit?
Ultimately this is the straw that stirs the drink within the industry and the question that needs to be answered. There are tremendous inefficiencies in the apparel industry today. Entire departments are working to manage supply chains and are striving to improve product quality. The departments are doing the costing of apparel orders with minimal data and legacy worksheets. The time to adopt digitalisation is now.
As described in a previous BST white paper, The MetaVertical Apparel Model, the Product Digital Twin incorporates 3D-simulation and animation that allows designers to model colour and fabric, as well as the performance of the assembled garment, thus minimising the need to prototype. So, what is the end result for the brand?
Imagine a fashion designer. Imagine materials, pattern, colour, and construction elements are added to a design and the designer has experience with the software that includes addressing the challenges and manufacturing feasibility of the garment design, live and in real-time. This digital twin product is made possible by a production that continuously evaluates the manufacturing capability and efficiency, providing insight into such issues as:
- Who can make this?
- How long will it take?
- How much will it cost?
- What is the expected level of quality?
- Is it made with sustainable manufacturing practices?
MetaVertical
With the data previously at the designers’ fingertips this information could determine the success of the line. Theoretically, the brand can predict the outcome of the order as it is being designed instead of reacting to the outcome months later as the factory. This is merely one example of how digitalisation, Industry 4.0 and digital twin technologies will create a paradigm shift in the apparel industry from ‘doing stupid faster’ to right the first time.
Black Swan Textiles and its partners are dedicated to solving this problem. Ultimately the advantages gained by having implemented this factory of the future is the paradigm shift the industry needs and allows for a MetaVertical approach to manufacturing in which on-demand and local production is for a local market.
In order to effectively deal with a fast-paced design process with a sensitivity to product cost, the apparel product development model must change. The same digital twin software that allows for 3D visualisation can be used to engineer the product, so that a manufacturing-ready specification can be communicated to the factory. In the digital twin process, a true specification will look different than the typical tech packs and bill of materials (BOMs) in play today. It includes the details required to drive manufacturing instead of development.
However, the apparel industry is not vertically integrated, so this type of data exchange does not take place. Brands share a globally dispersed manufacturing supply chain and each brand has different requirements for their factories – some of them manufacturing-related and some of them brand-related. So, the crux of the problem is that a fragmented supply chain must deal with different and ever-changing requirements from their customers.